- Home
- About
Flexible Packaging Films & Vacuum Bag Supplier
About Renature
Functional flexible packaging materials and packaging support for food vacuum packaging, flexible films and custom requirements.
Functional flexible packaging materials and packaging support for food vacuum packaging, flexible films and custom requirements.
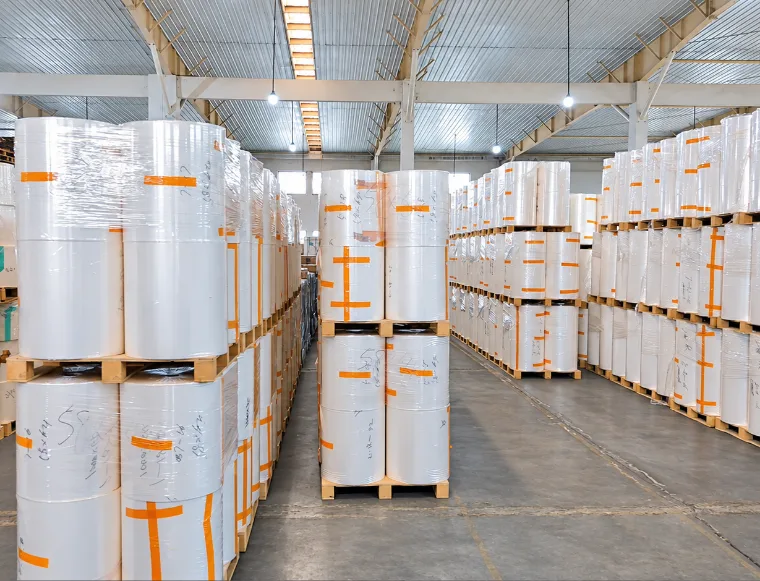
Renature New Material Technology Co., Ltd. is a professional brand focusing on functional flexible packaging. Our main products include high-barrier flexible films & pouches, vacuum packaging bags, packaging films, embossed vacuum rolls and bags, with customized development available according to customer requirements.
Backed by a mature backend manufacturing system, the company has professional R&D, testing and customer service teams.
An exclusive R&D and testing laboratory is equipped with a full set of testing instruments to carry out multi-dimensional performance tests on products.
We integrate the full chain of R&D, production, quality inspection and delivery.
With stable large-scale manufacturing capacity and end-to-end quality control, we provide reliable custom flexible packaging services and one-stop packaging solutions for global customers.
Shanghai Renature New Material Technology Co., Ltd. has grown around one product family: food packaging films and pre-made bags, together with the engineering and testing support that goes with them. Behind them stands a manufacturing base with over 20 years of experience in functional flexible packaging. The milestones of that path are set out below.
Sample timeline – to be replaced with Renature’s own milestones and dates.
Blown film, lamination and bag making begin in Shanghai.
Vacuum and shrink bags supplied to overseas meat and seafood processors.
Tensile, heat-seal, impact and barrier testing brought in-house.
BRC, ISO 9001 and Halal certification.
Every step of that path now stands behind one service: films and bags built to your specification, tested before they ship.
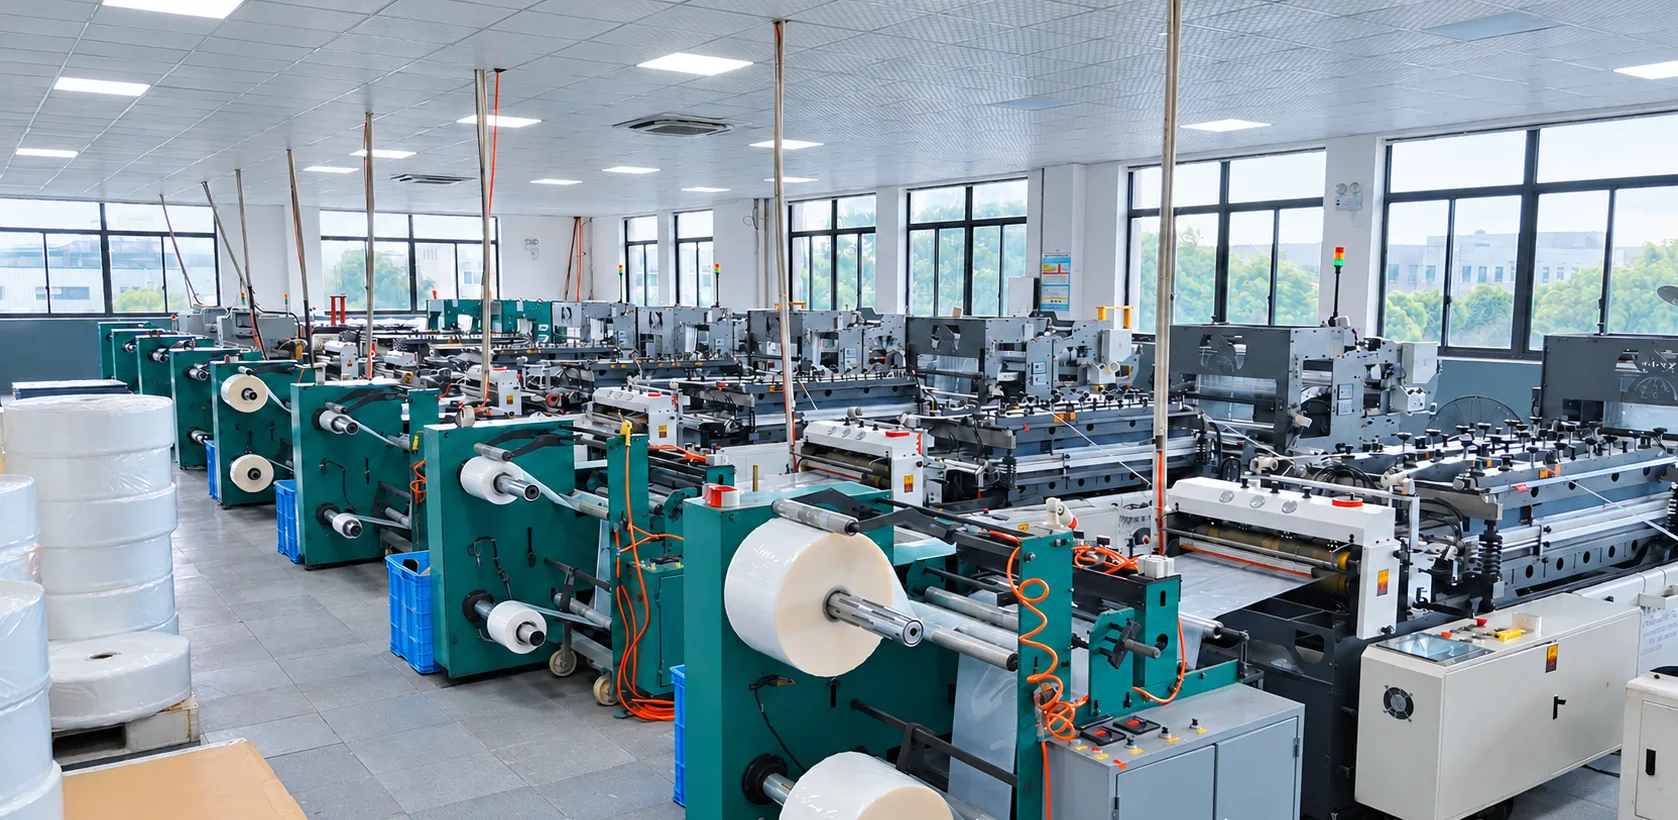
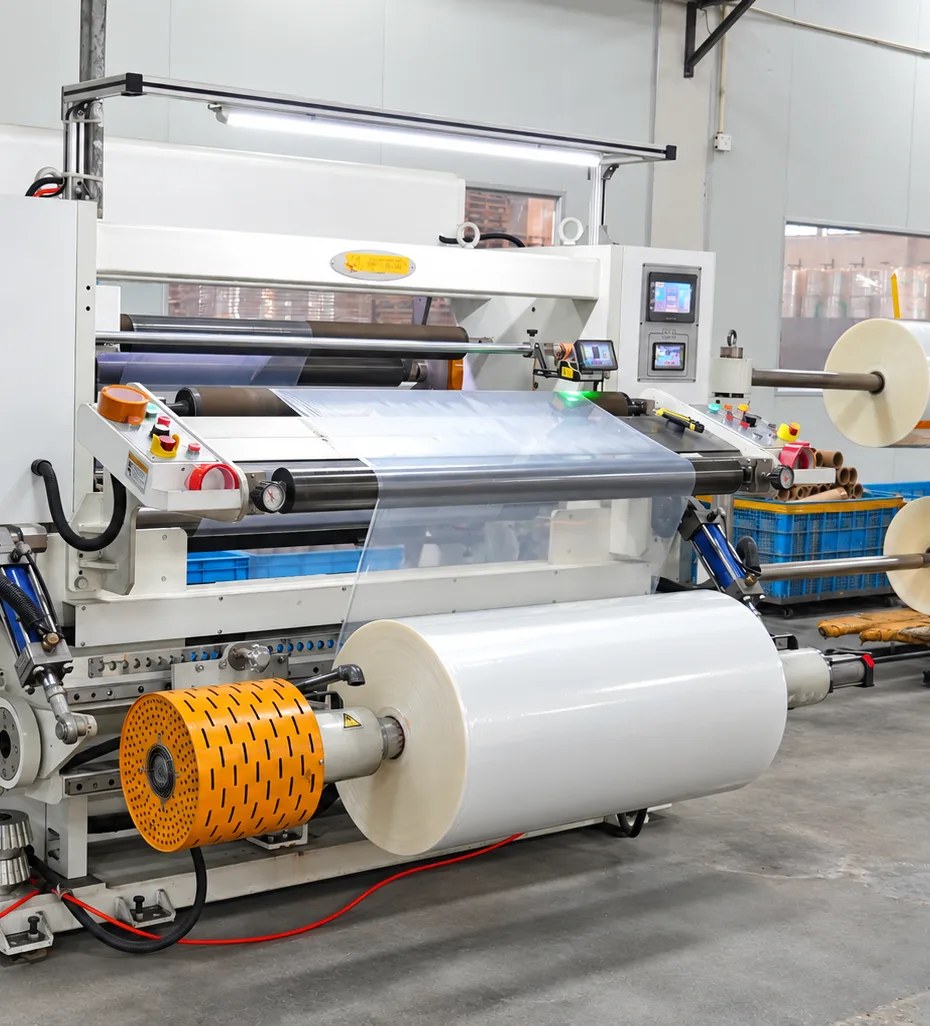
With over 20 years of experience in functional flexible packaging, our manufacturing base covers the complete processes of blown film, lamination, embossing, slitting and automatic bag making.
We can independently complete all operations from raw material forming to finished goods to meet customized and standardized production requirements for various high-barrier functional packaging products.
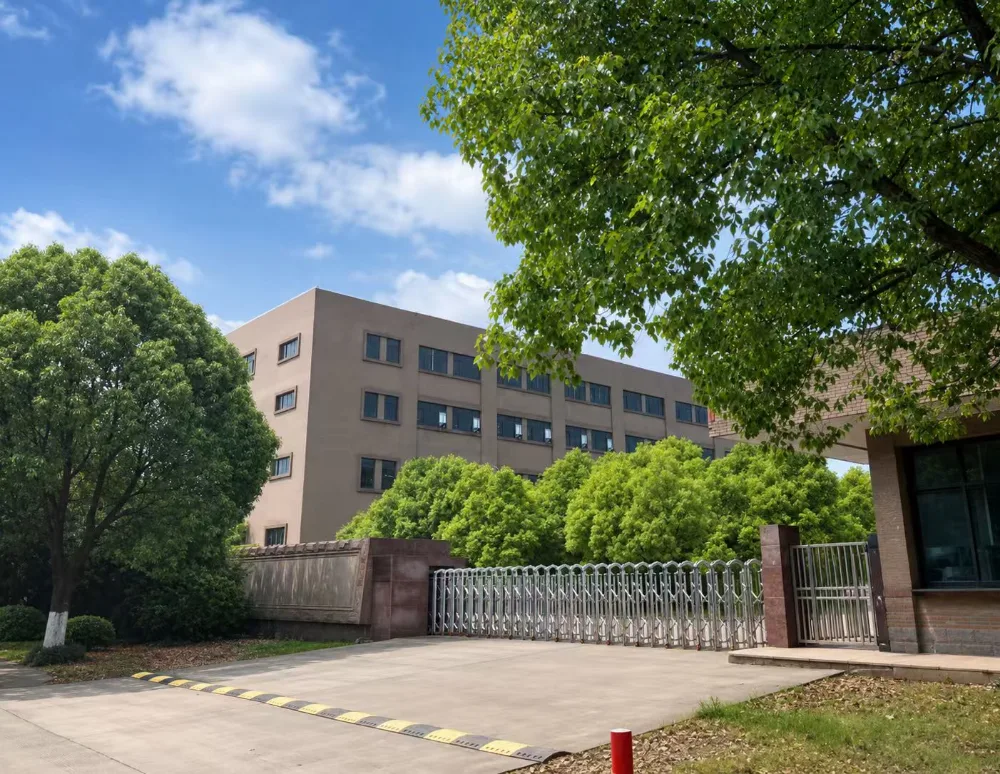 Production base
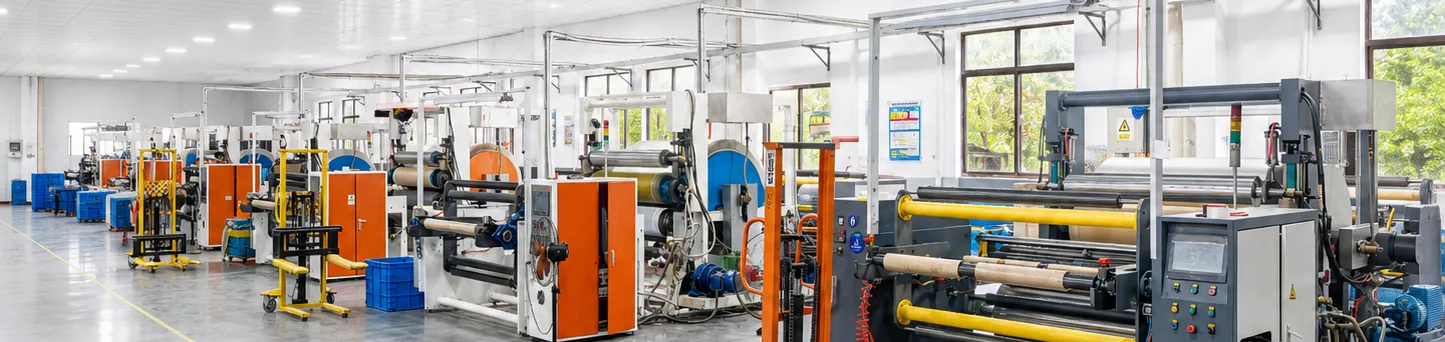 Converting hall
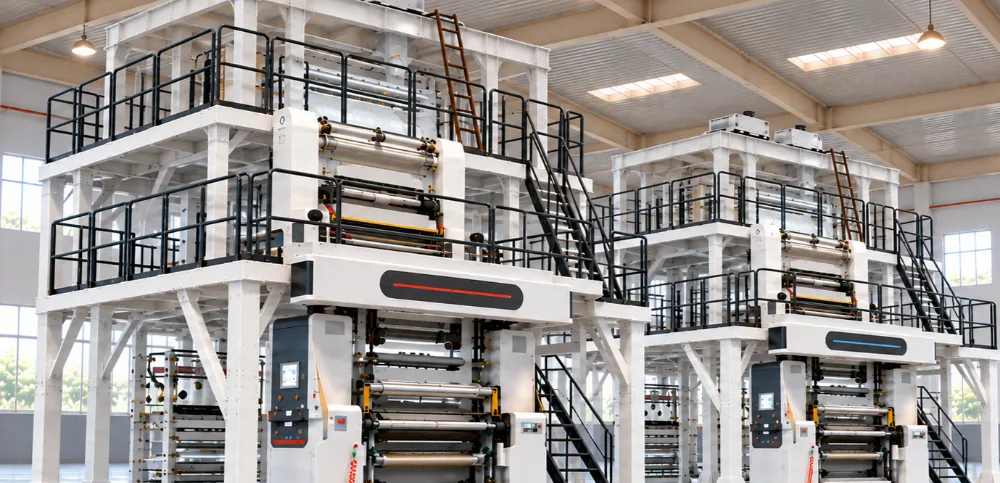 Co-extrusion lines
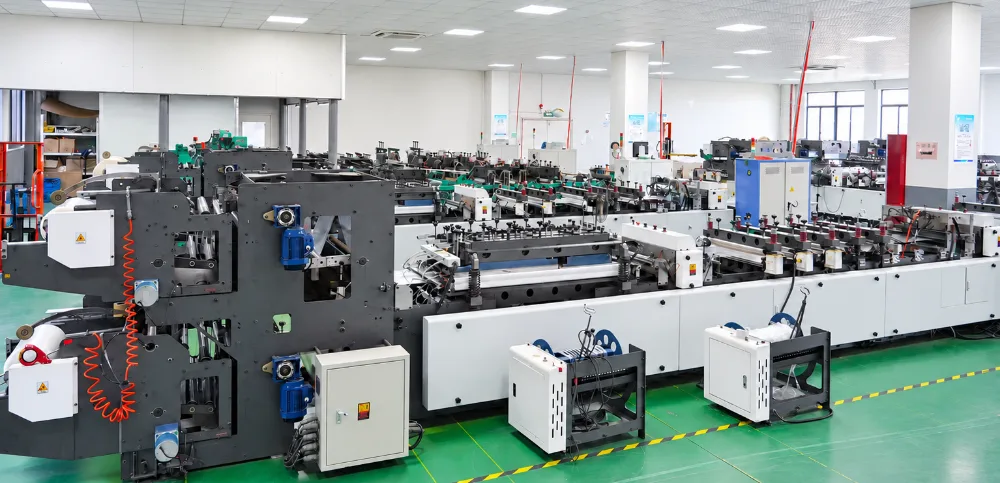 Automatic bag making
Multiple 9- and 11-layer co-extrusion blown film lines for high-barrier films, including 9-layer water-quenched blown film lines.
Complete in-house processes covering blown film, lamination, embossing, slitting and automatic bag making, from raw material forming to finished goods.
Multi-layer synchronous co-extrusion technology enables customized formulations and precise control of film thickness, layer structure and barrier performance.
Water-quenched EVOH films deliver excellent flatness, gloss, low haze and consistent quality for premium food packaging.
A company and factory overview: the production base, the workshop floor and the people behind RENATURE films and bags, in under a minute.
English subtitles. The film only starts when you press play, so sound stays off until you decide.
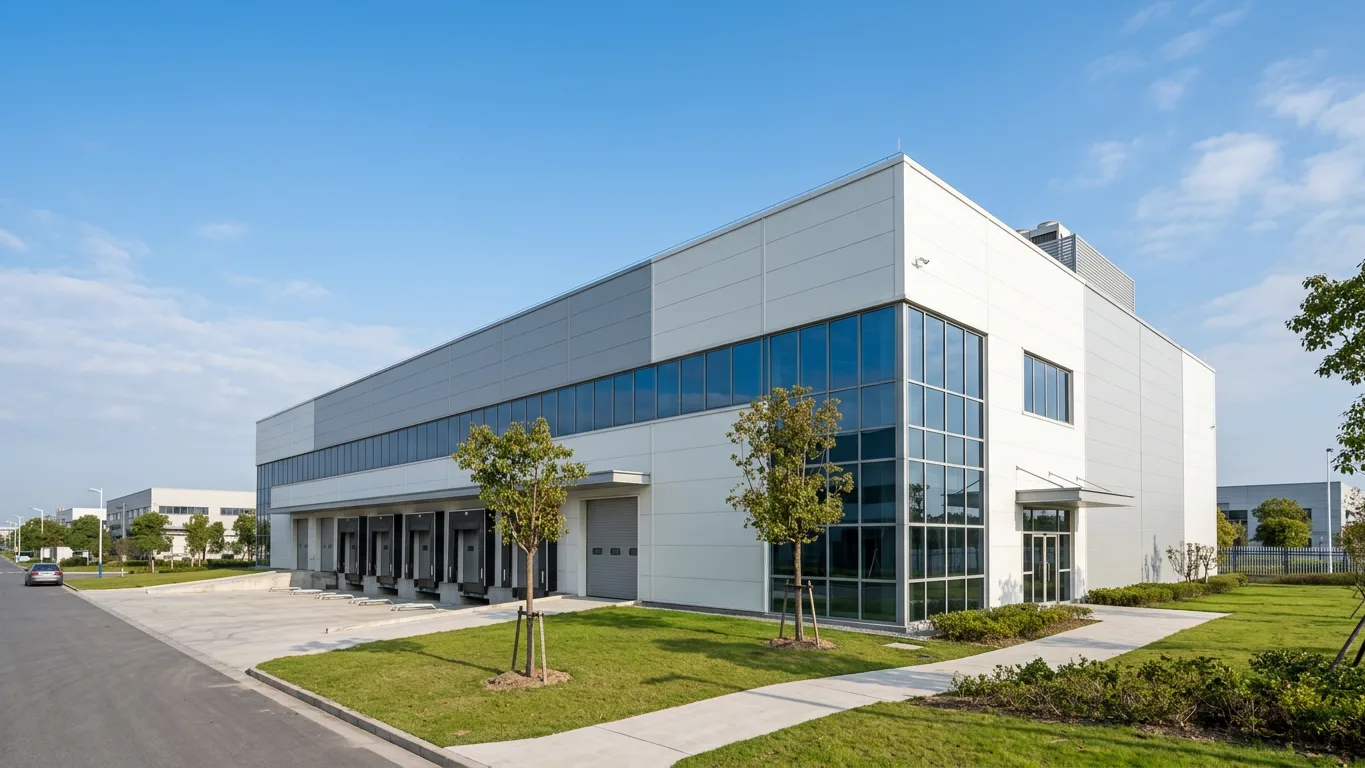
The company and factory film is being finalised. Our team can send you the current factory footage, or arrange a live video call through the plant, on request.
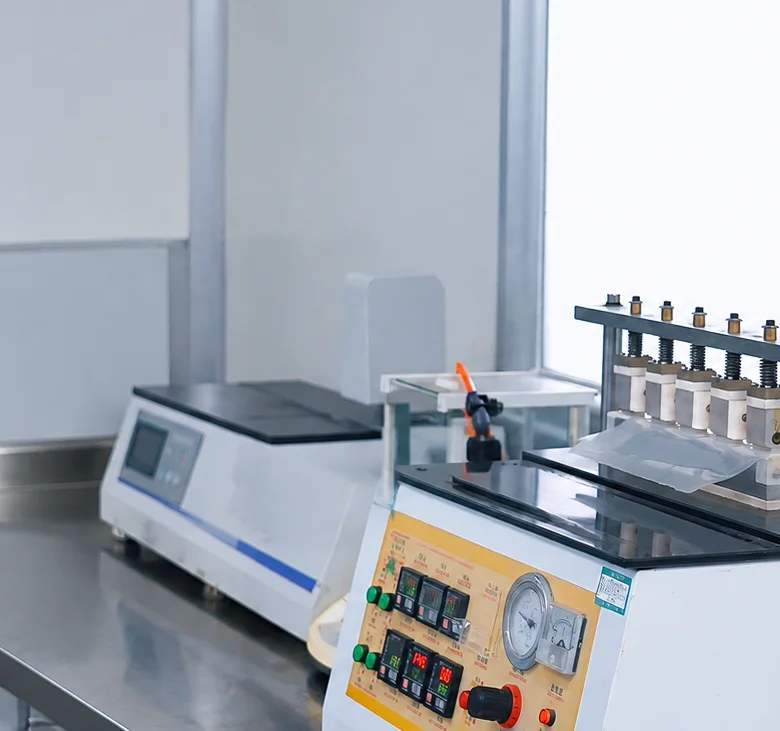 R&D and testing laboratory
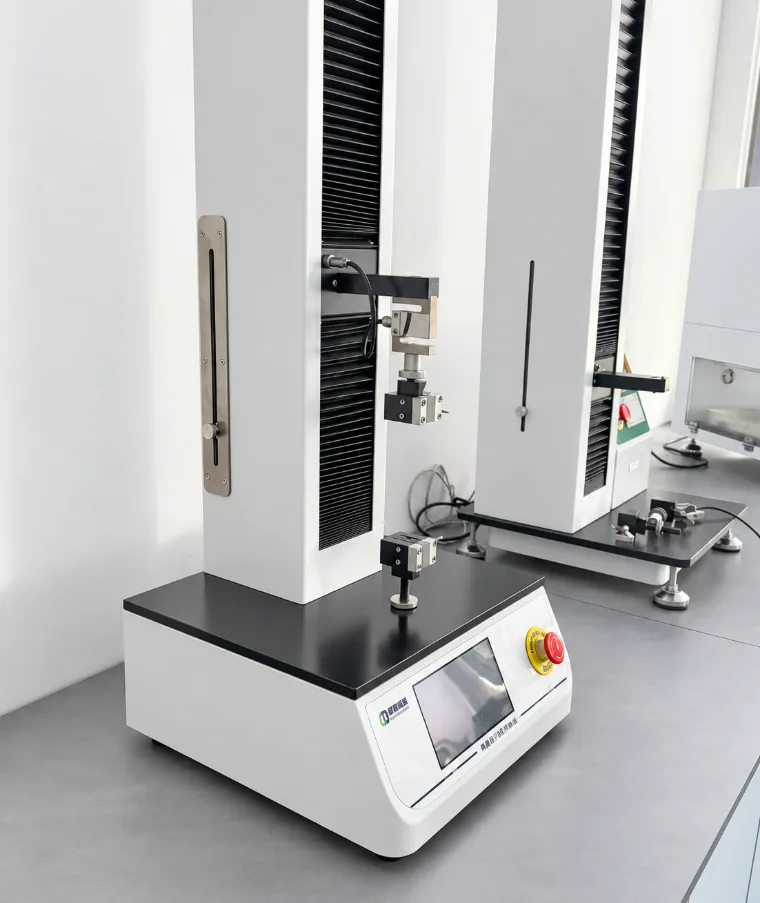
We implement full-process quality control from incoming raw material inspection and in-process monitoring to finished product release.

Strict control is applied to every working procedure to prevent non-conforming products from shipment.

Precision testing equipment supports standardized tests of barrier performance, sealability, tensile strength and film flatness.

On-line random inspection, in-process self-inspection and final product inspection are enforced during production.

Supported by stable technology and rigorous quality control, our products are steadily supplied to major European and American supermarket chains and e-commerce platforms.
From laboratory testing to production coordination and delivery assurance, our verified systems and collaborative teams support reliable customized flexible packaging solutions.
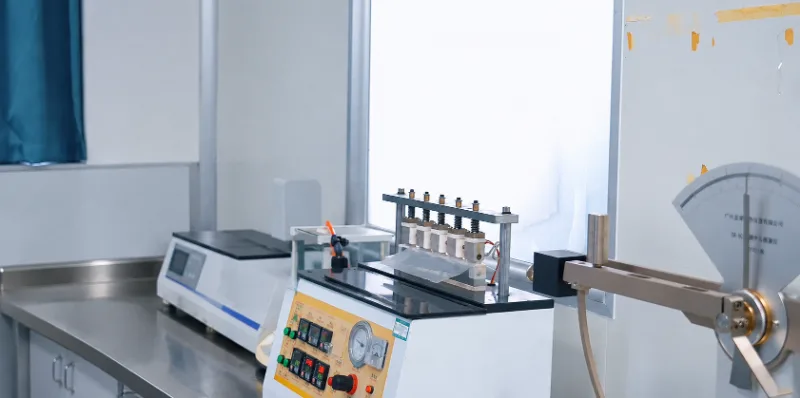

Precision equipment supports multi-dimensional testing and closed-loop quality control from raw materials to finished products.
EvidenceBarrier, sealability, tensile strength and flatness testing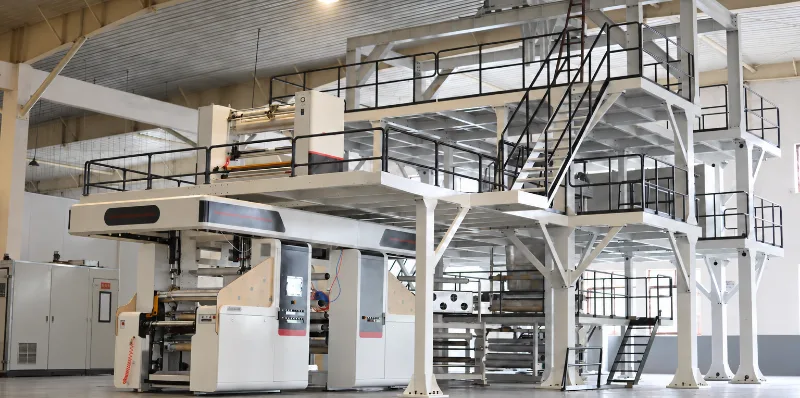

Standardized production and compliance systems support controlled manufacturing and food safety management.
EvidenceISO 9001 and BRC food safety standards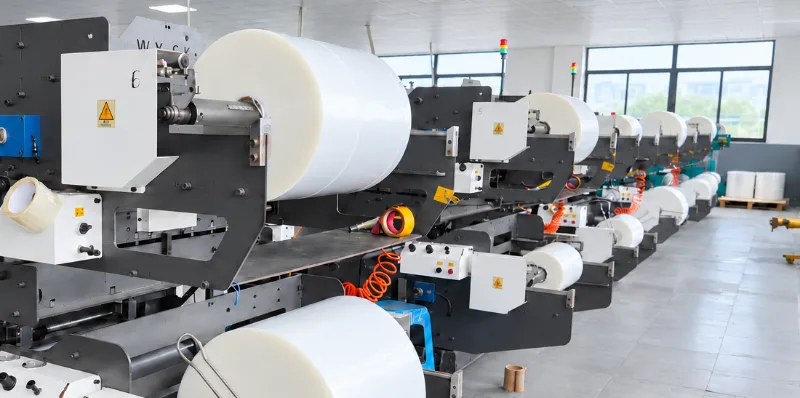

Products have passed SGS testing and meet applicable FDA food-contact requirements for domestic and international markets.
EvidenceSGS testing and applicable FDA food-contact requirements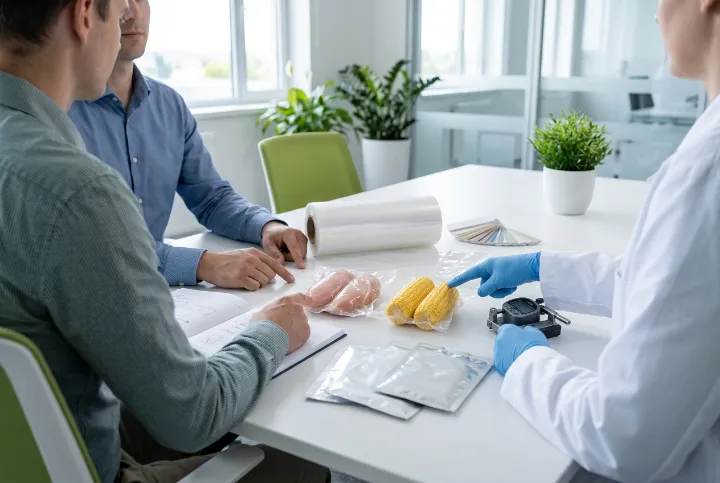

R&D, production, QC and customer service teams collaborate on product development, technical support, order tracking and delivery assurance.
EvidenceEfficient cross-team coordinationRenature works under third-party audited management systems. Certificate copies, patent details and food-contact test reports are shared with customers on request.

Details available on request.

Available on request for the relevant structures.
 Copy on request
Valid 2025–2026
 Copy on request
Certified 2025
 Copy on request
Certificate on file
Share the product, the machine and the volume. A packaging engineer replies with a proposal and, if useful, a sample plan.